Sliding DU Bushing Supplier: How to Evaluate Quality and Reliability for Your Application
2026-11-02
When a sliding DU bushing fails early, the root cause usually traces back to the supplier, not the design. But evaluating quality and reliability doesn’t have to be guesswork. From load capacity to lubrication pockets, a few focused checks can separate durable components from costly shortcuts. XIAYI has built its supply chain around these exact criteria, and this guide shows you what to look for before your next order.
Reading the Material Story Behind the Bushing
A bushing rarely gets a second glance until it fails, yet its material is a quiet archive of operating conditions. Porcelain bodies, epoxy-impregnated paper, silicone rubber sheds—each selection reflects a compromise between dielectric strength, mechanical stiffness, and long-term exposure to moisture and ultraviolet light. Manufacturing marks and subtle surface degradation often betray the real thermal and electrical stresses better than any nameplate rating.
To read that story, start with the interface where metal meets insulation. Hairline cracks near the flange or erosion tracks along the creepage path point to specific overload patterns. Even the choice of filler in a composite bushing can reveal whether the designer prioritized partial discharge resistance over ease of casting. Field inspections that note these details turn a passive component into a diagnostic tool, letting maintenance teams anticipate failures instead of reacting to them.
When Load Ratings Meet Real-World Demands
Load ratings printed on spec sheets rarely survive contact with a busy job site. A caster stamped for 800 pounds was almost certainly tested on a smooth, level floor with a perfectly centered load. Shift that same weight to one edge, add a cracked concrete joint, and push the cart over it a few dozen times an hour, and the forces spike well past the lab numbers. Real-world demands include shock, vibration, uneven weight distribution, and temperature swings, none of which fit neatly into a single static figure.
That gap between nominal capacity and actual stress is where equipment gets pushed past its limits. Engineers often apply a safety factor, but even a generous one can be undermined by dynamic loading conditions. A conveyor roller that handles 300 pounds at rest might see momentary loads two or three times higher when packages drop onto it from even a short height. Repeated impact and fatigue then shorten service life in ways a single load test never reveals.
Field observation and real-time load monitoring tend to tell a more honest story than any catalog rating. When operators track how a wheel, bearing, or frame behaves under daily abuse, they can adjust their selection, add reinforcement, or change maintenance intervals before something fails. The lesson is straightforward: load ratings are a starting point, not a guarantee, and only real-world use reveals the true working margin.
Surface Finish and Tolerances That Separate Precision from Guesswork
In high-stakes machining, the difference between a part that fits perfectly and one that needs a hammer often comes down to two numbers: the specified surface roughness and the tolerance band. A finish average of Ra 0.8 µm might look polished to the naked eye, but under a profilometer it reveals the subtle peaks and valleys that control how seals seat, how lubricant spreads, and how two mating surfaces wear over time. Likewise, a tolerance of ±0.005 mm on a bearing journal isn't just a drawing annotation—it's the boundary between a press fit that holds for years and a sloppy assembly that loosens after fifty cycles.
Experienced shops treat these specs as a system rather than isolated targets. A tight diameter tolerance with a rough turned finish is often wasted, because the surface peaks will quickly flatten and alter the effective size under load. Conversely, a mirror-like surface on a non-critical cosmetic edge adds cost without function. The real separation from guesswork happens during process planning: selecting the right grinding wheel grit, adjusting feed rates to avoid chatter marks, or using honing to correct both geometry and surface texture simultaneously. This requires hands-on verification with calibrated equipment—not just trusting a CAM simulation to deliver what the blueprint asks for.
When tolerances drop below ±0.002 mm or finishes demand Ra 0.2 µm, thermal growth and vibration become the enemy. A spindle warming up can shift a feature by more than the total tolerance, so stable temperature control and in-process measurement are non-negotiable. Shops that separate precision from guesswork document their measurement uncertainty, cross-check with air gauges or CMMs, and adjust tool wear compensation based on real data rather than intuition. That discipline turns a printed tolerance into a repeatable physical result, not a hopeful estimate.
What a Supplier's Test Data Actually Reveals
Supplier test data often gets treated like a rubber stamp, but it can hide more than it shows. The numbers reflect only the conditions the supplier chose to run, not necessarily the ones you care about. If a batch looks too consistent, that itself is a signal worth investigating.
Dig into the margins. A supplier may report pass/fail thresholds, but the actual distribution of measurements tells you whether the process is centered or drifting toward a cliff. Test data rarely lies outright; it just fails to mention the outliers, the retests, and the fixtures that were adjusted mid-run.
Compare repeated test reports over time. Shifts in standard deviation, changing test methods, or missing data from certain dates can reveal more about the supplier's quality system than any certificate. What's absent often matters more than what's printed.
Field Failures Speak Louder Than Spec Sheets
A spec sheet will tell you an enclosure survives a four-foot drop onto concrete. It won’t mention the technician who drops it twice a week from a bucket truck, then leaves it in the rain overnight. We track every returned unit, strip it down, and map each failure back to a real job site. Those patterns matter more than any lab report.
Some of our biggest design changes came from field failures that looked minor on paper: a gasket that held in a dust chamber but let fine silica in after 900 hours of vibration, a connector that passed salt spray but corroded after repeated mating with oily gloves. When a part fails in use, we don’t dismiss it as misuse. We redesign the weak point and run our own accelerated tests until the failure rate drops to near zero.
You’ll rarely see those details in glossy marketing copy. But ask any field engineer what they trust, and they’ll tell you about the model that survived three years of abuse before needing a new latch, not the one with the most impressive IP rating on paper. That’s why our internal failure database drives every new revision. If a real-world failure is louder than a spec sheet, we’d rather listen to it early.
Custom Geometry and Support Beyond the Catalog
When standard profiles fail to meet the demands of a load-bearing frame or a space-constrained assembly, the real work begins in geometry that was never drawn in a catalog. We regularly adjust web thickness, flange width, and bend radii to shift the neutral axis or gain a few critical millimeters without adding weight.
The same thinking applies to the support we offer around those custom sections. Instead of handing over a drawing and ending the conversation, our engineers stay involved through prototype validation, surface finishing, and tolerance stacking. That often means a revised slot pattern here, a non-standard hole placement there, or a rapid second iteration when the first test assembly reveals an interference nobody predicted on screen.
Because these geometry tweaks are rarely isolated, we treat each request as a small engineering project rather than a one-off order. The result is a part that fits your assembly the first time and a support path that continues until the production run is stable.
FAQ
Ask both to run a side-by-side wear test under your actual load and speed, not theirs. The one who hesitates or only offers a generic brochure probably has something to hide. Also check the surface roughness of the bronze layer—if it feels patchy to the touch, the PTFE won't embed evenly and you'll see early scuffing.
The bore tolerance after press-fit is the one that bites you later. A supplier should provide the recommended housing bore and shaft tolerance together, not just a bushing OD. If they can't tell you what the running clearance should be after installation, they're just reselling stock sleeves.
Yes, request a sample and have a local shop cut it in half, then try to peel the bronze layer with a knife. It should resist peeling and show a clean, uniform interface. If it lifts easily or you see gaps at the edge, the sintering step was rushed.
Lead-free variants usually run a little warmer and can be less forgiving with marginal lubrication, but the gap has narrowed a lot. If you work in food or water contact, go lead-free, but ask for PV data at your operating temperature—don't assume the same load rating carries over.
A real supplier will send you a mill certificate with batch numbers, a surface roughness trace, and full dimensions measured on a CMM or optical comparator. If you only get a one-page PDF with a logo and a photo of a bushing, treat that as a warning sign.
Ask about their sintering furnace and what temperature profile they use for the bronze layer. A trader will go silent or give a vague answer. A manufacturer can tell you the dwell time, atmosphere, and how they control porosity—those details can't be faked easily over the phone.
If your application has a tight ramp-up or you need oddball sizes, the shorter lead time and easier communication usually pay for the premium. For a steady, standard-size, high-volume part, imported bushings can be fine if you have the inspection capacity to catch bad batches early.
Watch for a rapid rise in friction after a short break-in period, or brownish streaks on the shaft. Those usually mean the PTFE layer has worn through unevenly or the bond is failing. Also, if you see iron filings around the bushing edge, the steel backing is galling, which points to misalignment or a badly finished bore.
Conclusion
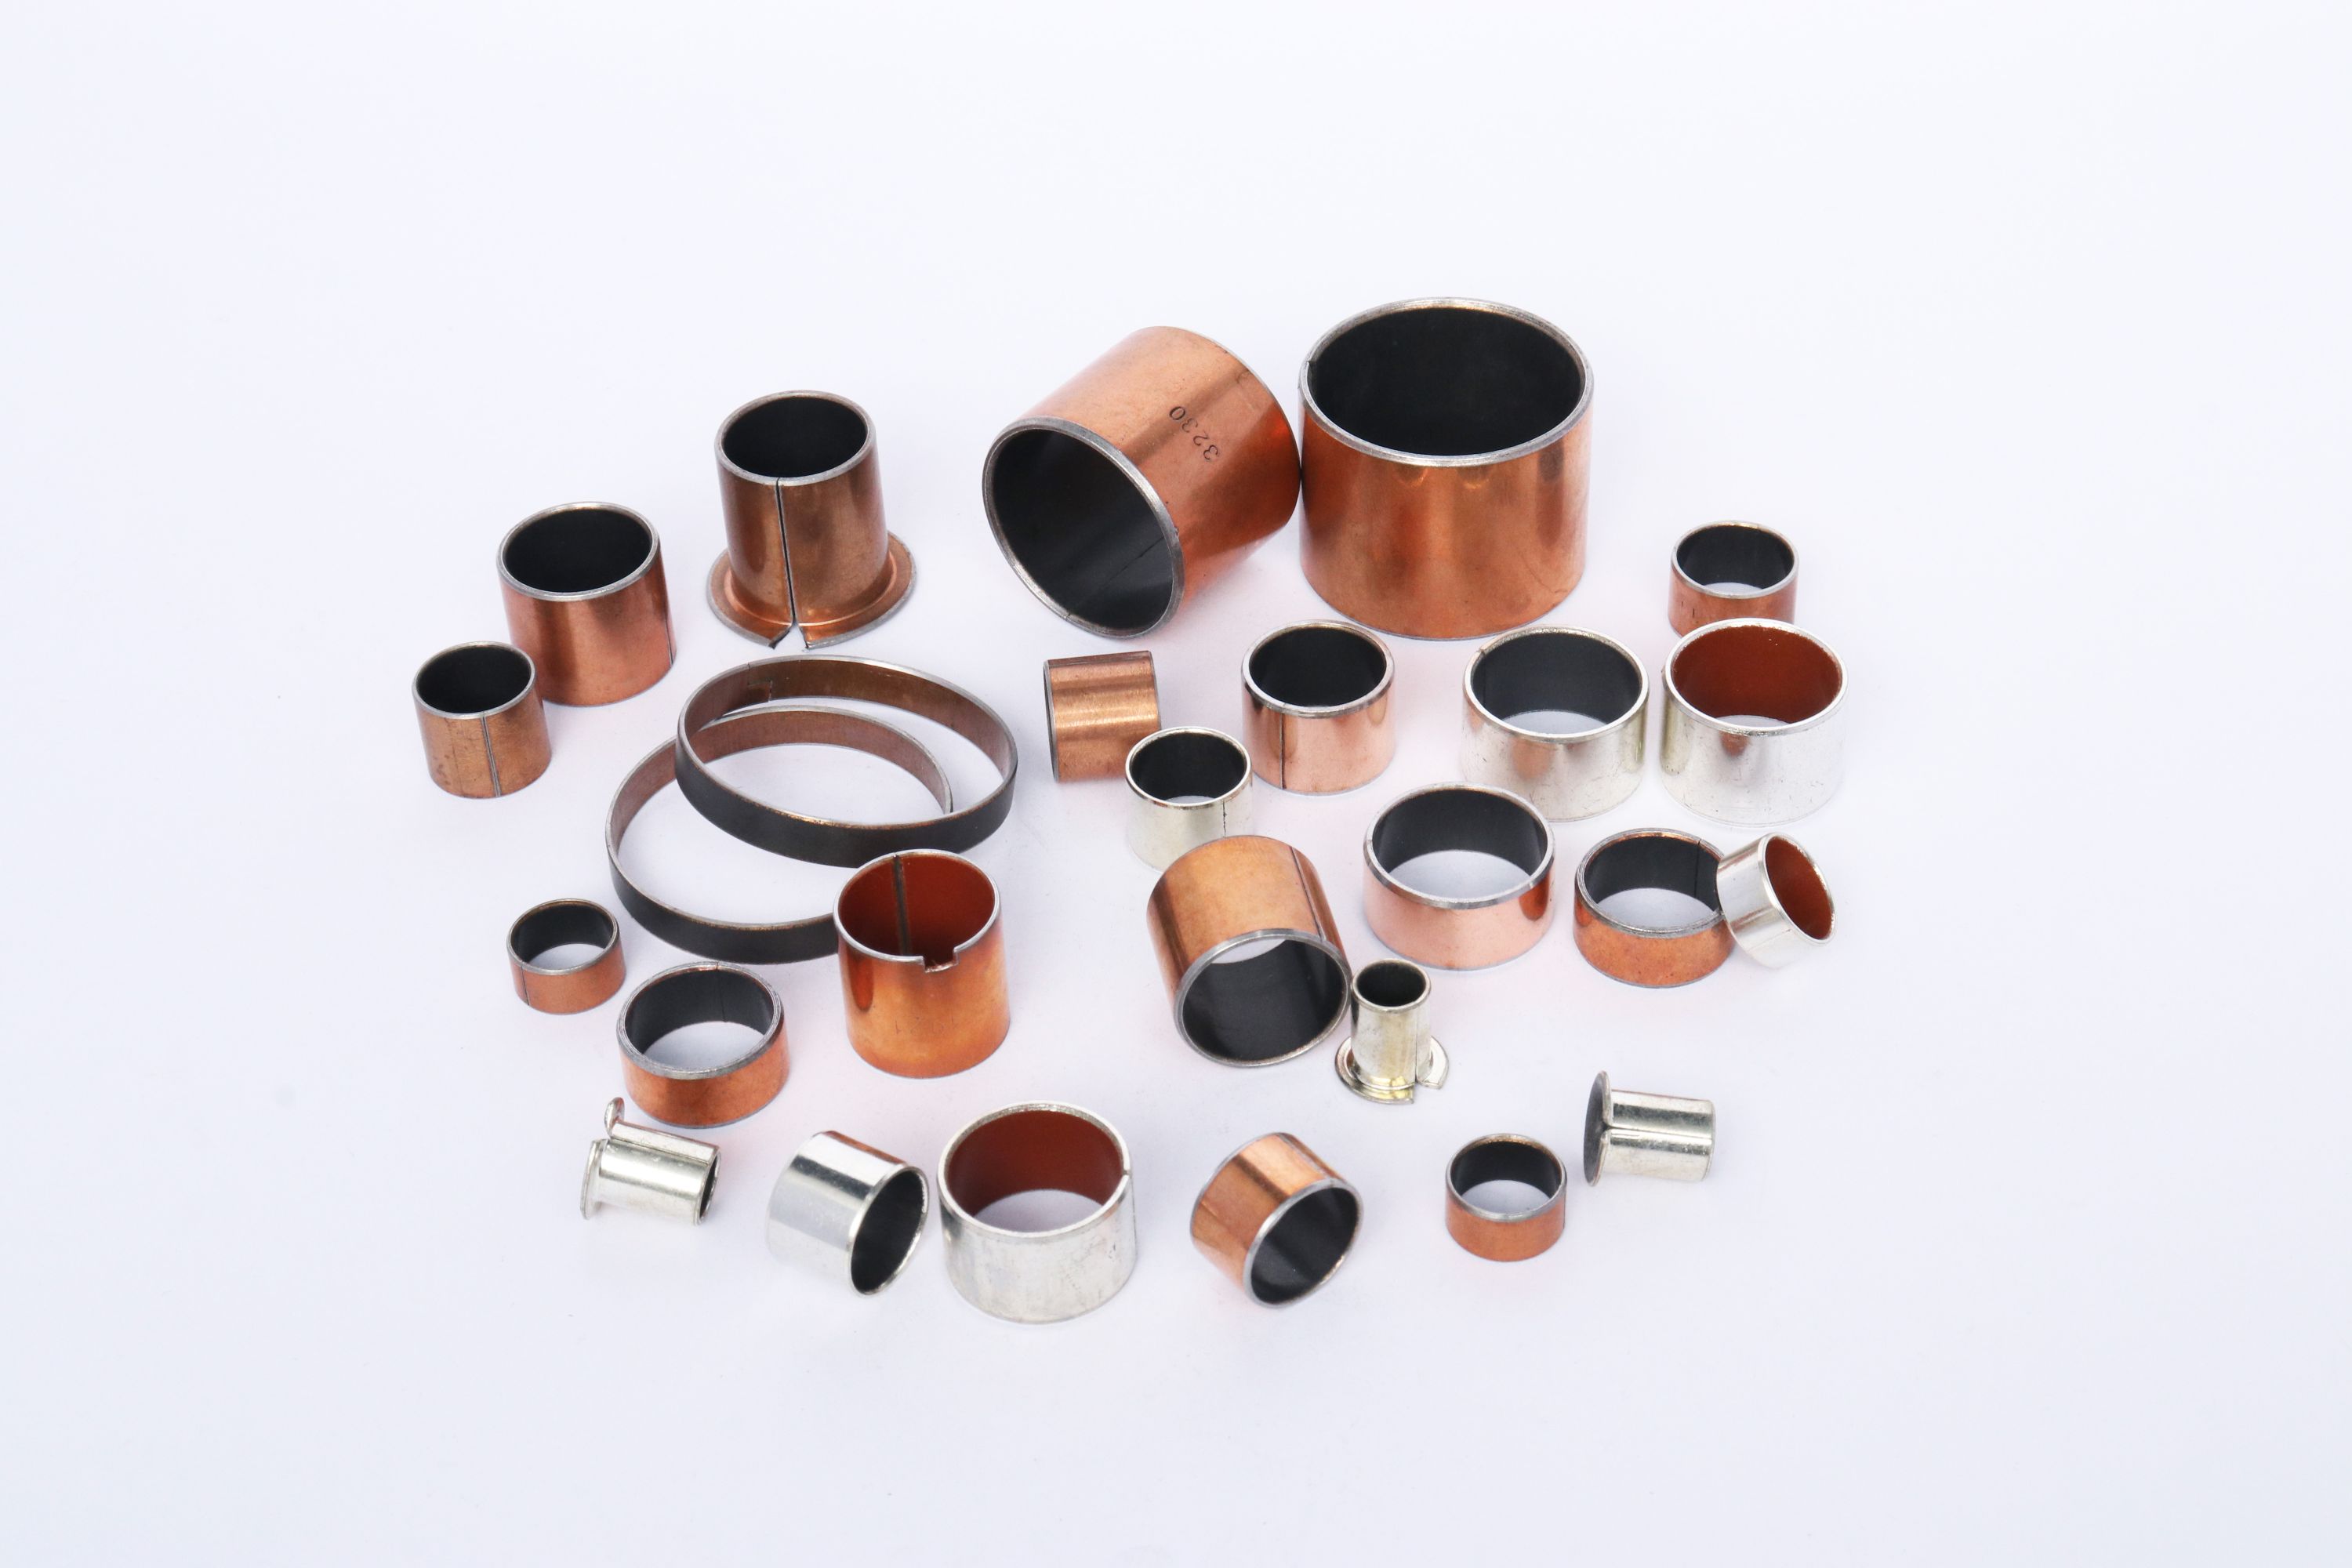
Evaluating a sliding DU bushing supplier demands more than a glance at catalog pages. Start by digging into the material story—most DU bushings pair a steel backing with a sintered bronze layer and a PTFE/lead overlay, but the exact powder composition, sintering temperature, and impregnation method vary widely between suppliers and directly shape wear life under load. Load ratings, too, need to be matched to real-world conditions: edge loading, intermittent motion, or vibration can invalidate a static load number that looks impressive on paper. Surface finish and tolerances separate the serious manufacturers from guesswork. A bushing with a rough ID or out-of-round cross-section will chew through the polymer layer long before its rated hours. Ask for actual test data from bench setups that mimic your operating envelope—temperature, speed, and mating surface—not just a polished sample report.
Field failures speak louder than spec sheets, so request case studies or failure analyses from similar applications. A supplier who openly discusses past root causes and corrective measures is more trustworthy than one who hides behind warranty language. Custom geometry and support beyond the catalog also matter: a good supplier will modify the bushing length, add grease grooves, or adjust interference fit for your housing, and their engineers should offer installation guidance to prevent misalignment or damage during press-fitting. Ultimately, reliability comes from combining material insight, realistic testing, and responsive problem-solving—not from a single impressive number on a datasheet.
Contact Us
Contact Person: Leela
Email: [email protected]
Tel/WhatsApp: 8613586885132
Website: https://www.xiayishockparts.com